If a quote comes in higher than expected, this article explains why and how to reduce the cost of the next one.
The five factors that move a quote
1. Part volume (not bounding box) Pricing is driven by the actual volume of material your part uses, not its bounding box. A hollow shell prints for a fraction of the cost of a solid block with the same outer dimensions. Hollowing and infill are the largest cost levers on FDM.
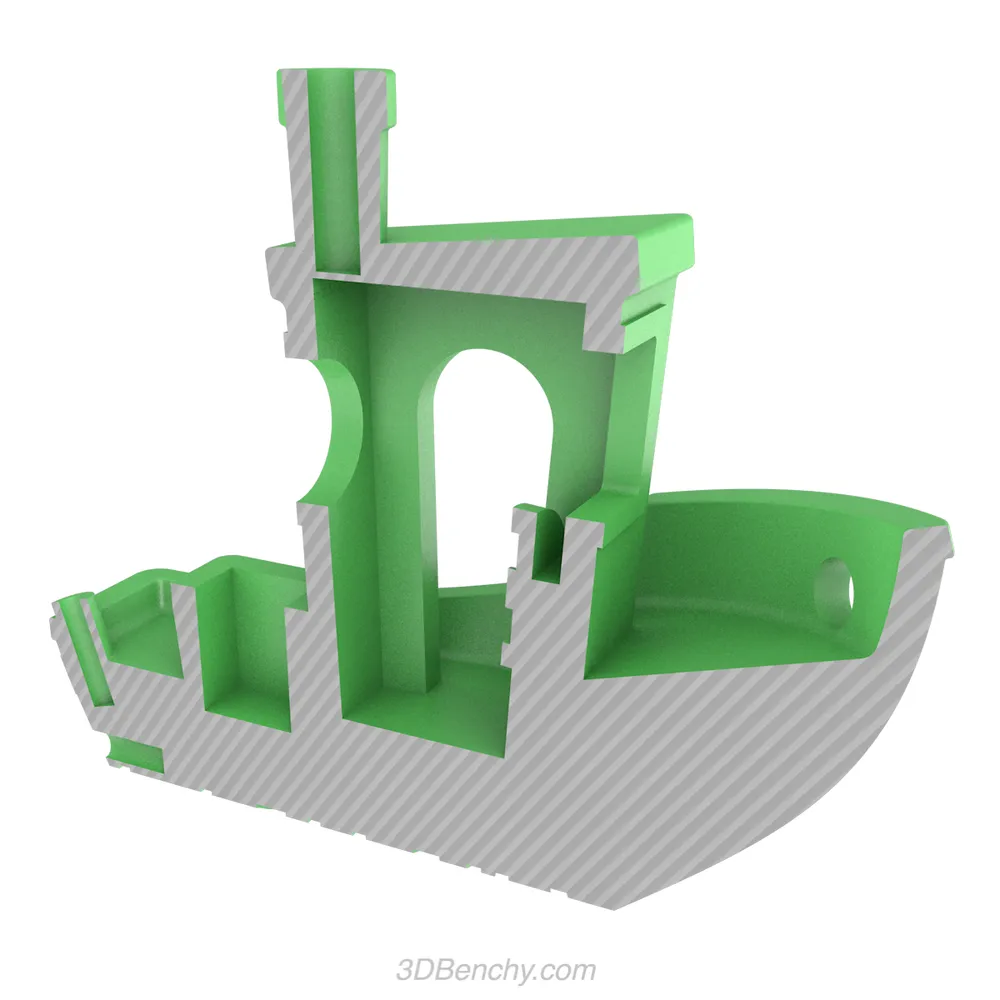 Most prints are a solid skin around a light 'infill', which is why size alone does not set the price. Image: CreativeTools, 3DBenchy, CC0, via Wikimedia Commons.
2. Material PLA is the least expensive. PETG, ABS, and standard resin sit in the middle. Engineering materials (nylon, polycarbonate, carbon-fibre-filled, dental or high-temperature resins) cost several times more per gram. Choose the least expensive material that meets your functional requirements.
3. Technology FDM is the least expensive per cubic centimetre and suits functional prototypes and large parts. SLA (resin) costs more and gives a smooth surface finish and fine detail. Match the technology to the use.
FDM and resin (SLA) are the two technologies our makers run. Powder and metal processes (SLS, MJF, DMLS) are described in our technology guides as general industry reference. We do not currently fulfil them.
4. Post-processing Raw prints are the least expensive finish. Sanding, priming, painting, vapour smoothing, dyeing, and threaded-insert installation each add labour. Request only the finishes the part needs.
5. Turnaround Each quote states its own delivery date. Where a maker can offer a faster turnaround, it is priced into their quote.
How to obtain a lower quote without lowering quality
- Upload the same file and request quotes in both FDM and resin to see the difference.
- Reduce infill on FDM parts to 15–25% unless you need structural strength.
- Print more units in one batch; the fixed setup cost is spread across them.
- Split large parts into smaller pieces that fit smaller machines, then join them.
- Accept standard colors (natural, black, white); custom colors add material-change time.
What does not save money
- Requesting "no supports" on SLA. The slicer adds them automatically; design overhangs below 45° where you can.
- Requesting a "rough finish". A raw print off the plate is already the least expensive finish.